Part 2: Body — A Thousand Small Operations Behind Every Tank
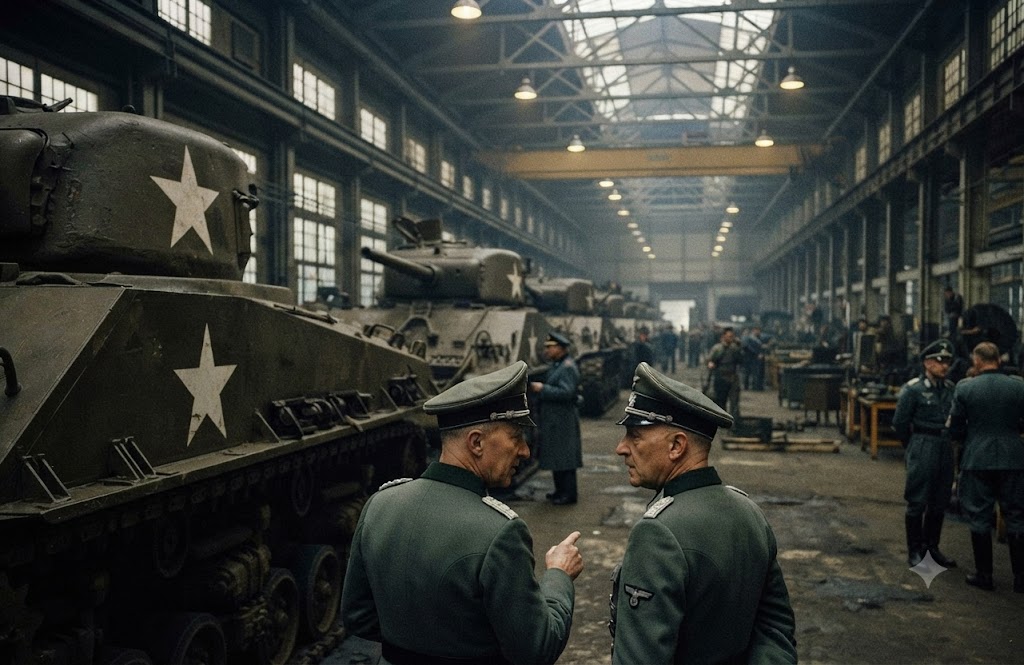
Inside the factory, the generals entered a vast production hall illuminated by rows of overhead lamps.
The air was thick with heat, oil, and the smell of freshly cut metal. Overhead cranes carried heavy components from one station to another. Workers guided steel plates into position while technicians inspected measurements and checked mechanical assemblies.
There was no single craftsman laboring for weeks to complete an entire vehicle.
Instead, the work had been divided into hundreds of coordinated operations.
One team prepared hull sections. Another installed suspension components. Elsewhere, workers assembled engines, fitted electrical systems, and prepared turrets. Each section moved toward the next station according to a carefully organized schedule.
Von Keller stopped beside a half-assembled tank.
“Who designed this production system?” he asked.
“Engineers, factory managers, and production specialists,” replied the American guide. “The system developed through experience. We change it whenever we find a way to reduce delays.”
The German general examined the hull.
“And how many skilled workers are required to complete one vehicle?”
“Not every worker needs to be an expert in every part of the process. We train people for specific operations, establish standards, and inspect the results.”
Von Keller said nothing.
German factories could produce highly sophisticated machinery, but their wartime industrial system faced mounting problems. Allied bombing damaged factories and transportation networks. Shortages of fuel and raw materials disrupted production. Different vehicle designs demanded different parts, maintenance procedures, and manufacturing methods.
German industry still produced formidable equipment, but the increasing pressure of the war made every complication more costly.
The American factory presented a different challenge to German assumptions.
Its strength did not depend entirely on a single brilliant engineer or an extraordinary machine.
It depended on coordination.
The group moved to another section, where engines were being tested before installation. A technician checked a series of readings, marked a production card, and directed an engine toward the next station.
A German general leaned toward von Keller.
“They are treating engines like interchangeable components.”
“Within established specifications,” von Keller replied. “That is precisely what makes the process possible.”
For the first time that morning, the older officer sounded less dismissive than curious.
Then the guide led them toward a large window overlooking the shipping yard.
Rows of completed tanks stood ready for inspection. Railway cars waited on nearby tracks. Trucks carried crates of spare parts toward loading areas, while other vehicles transported tools and equipment required by maintenance units.
The guide explained that manufacturing a tank was only one part of the problem.
The vehicle also needed ammunition, fuel, trained crews, replacement tracks, engines, repair facilities, and a reliable supply route to the battlefield.
“A tank that cannot move is a steel box,” he said. “A tank that cannot be repaired is a temporary advantage. We have to think about the entire system.”
General Otto Reinhardt, who had commanded armored formations on the Eastern Front, frowned.
“Your Sherman is not superior to every German tank in armor or gun performance.”
“That’s true,” the guide answered. “No vehicle wins every comparison. But a tank’s battlefield value depends on more than its specifications.”
He pointed toward the shipping yard.
“If one vehicle is damaged, we need to recover it, repair it, or replace it. If a unit loses several vehicles, replacements must reach it quickly. If an engine fails, mechanics need the correct parts. Our production system is designed to support those needs.”
Reinhardt looked away.
He remembered German crews waiting for replacement components that never arrived. He remembered vehicles abandoned because a relatively small mechanical failure could not be repaired under battlefield conditions. He remembered commanders conserving their remaining armor because they knew that losses might never be replaced.
The American officer continued.
“Our factories don’t win battles by themselves. Soldiers, logistics personnel, mechanics, and commanders still have to do their jobs. But industrial capacity gives them options.”
They proceeded to a production office overlooking the assembly floor. Large charts displayed manufacturing targets, delivery schedules, and inspection results. Supervisors moved between desks, discussing delays and reallocating materials.
A young American engineer explained that production rates varied by factory, model, and period. The plant had to account for maintenance, component shortages, changing military requirements, and quality-control failures.
One German officer interrupted.
“We were told your factories could build a hundred tanks every day.”
The engineer paused.
“Not every factory, and not every day. Different plants produced different vehicles, and output changed over time. But American industry could manufacture armored vehicles in enormous numbers across multiple facilities.”
He pulled a report from a folder and placed it on the desk.
The generals gathered around.
The figures showed how American wartime manufacturing had expanded through coordinated work among government agencies, private companies, subcontractors, and transportation networks.
The United States did not need every factory to produce one hundred tanks daily. Its advantage came from the combined output of an industrial system operating across the country.
The generals studied the report in silence.
Their guide then led them to a maintenance demonstration. A damaged tank had been positioned inside a repair bay. Mechanics removed worn components, examined the transmission, and prepared replacement parts.
The process was methodical rather than theatrical.
There were no speeches about American superiority. No one mocked the prisoners. The workers simply continued doing their jobs.
Von Keller watched a mechanic compare a damaged component with a replacement before signing an inspection sheet.
“How long would this repair take?” he asked.
“It depends on the damage, the availability of parts, and the workload,” the mechanic replied. “We try to make the repair predictable, not leave it entirely to improvisation.”
The answer unsettled the general more than a boast would have.
He had spent his career studying battles, calculating fuel requirements, estimating enemy strength, and searching for tactical advantages. He had believed that a well-designed machine, operated by a well-trained crew, could alter the course of an engagement.
Now he was confronting a larger calculation.
Germany could build a powerful tank. But could it produce enough tanks, maintain them, move them across a collapsing transportation network, and replace its losses while fighting enemies on multiple fronts?
By 1945, the answer was increasingly clear.
Reinhardt finally turned toward the American officer.
“Tell me something. If your tanks are not individually superior in every respect, why did our commanders fear your industrial strength so much?”
The officer considered the question.
“Because a battle doesn’t end when one tank is destroyed. There are more questions afterward. Can the enemy replace it? Can he supply the next formation? Can he keep his factories running? Can he move equipment where it is needed?”
He glanced across the production floor.
“We cannot promise to win every battle. But we can make sure our forces have the equipment and support to keep fighting.”
Von Keller looked through the window again.
The factory seemed almost endless.
He had once believed that Germany’s military future depended on producing exceptional weapons and employing them with exceptional skill. He had underestimated how devastating a sustained imbalance in production, transport, and replacement capacity could become.
His country’s defeat had not been caused by one factory or one type of tank. It had emerged from many interconnected failures: strategic decisions, the burden of fighting multiple enemies, shortages, bombing, fuel constraints, and the growing inability to sustain military operations.
Yet this factory gave those failures a physical shape.
He watched another completed tank move toward inspection.
For the first time, von Keller understood that the American advantage was not simply the number of vehicles standing outside.
It was the system that had made those vehicles possible.
Part 3: Conclusion — The Lesson No General Could Ignore
Late that afternoon, the German prisoners returned to the truck.
The sun was beginning to sink behind the factory roofs. Workers continued their shifts, and freight cars rolled toward the railway junction. The plant showed no sign that a group of defeated generals had spent the day examining its operations.
General Reinhardt climbed aboard and sat beside von Keller.
“You know,” he said quietly, “I used to think our greatest advantage was that we understood war better than our enemies.”
Von Keller watched the factory disappear behind the trees.
“Perhaps we understood certain parts of it.”
Reinhardt turned toward him.
“And the rest?”
“The rest kept arriving in railway cars, spare parts, fuel deliveries, replacement engines, and new crews.”
Neither man spoke for several minutes.
They had commanded armies whose reputations rested on speed, discipline, tactical skill, and the quality of their equipment. They had witnessed German engineers create machines that demanded extraordinary technical ability. Some German vehicles were formidable weapons, and the generals had no reason to pretend otherwise.
But technical excellence could not erase the consequences of an industrial and logistical imbalance.
The Americans had demonstrated that military power extended far beyond the battlefield. It depended on factories capable of maintaining output, transportation systems capable of moving equipment, workers capable of repeating complex operations, and supply networks capable of sustaining distant armies.
Germany’s military leaders had often sought a decisive advantage through superior weapons or operational breakthroughs. Yet even successful operations could not permanently solve the problem of replacing losses while the enemy continued to replenish his forces.
The factory had not proved that every American tank was better than every German tank.
It had revealed something more consequential.
A country did not need to produce the most sophisticated weapon in every category to build overwhelming military capacity. It needed to combine effective equipment with sufficient numbers, reliable maintenance, trained personnel, and a system capable of keeping everything moving.
As the truck approached the prisoner camp, Reinhardt asked one final question.
“Do you think we could have built the same system?”
Von Keller considered it carefully.
“Perhaps parts of it. But not simply by copying their factory floors. We would have needed different priorities, different production decisions, secure transportation, dependable supplies, and time.”
He paused.
“And by the time we understood how much time we needed, we no longer had it.”
The truck passed through the camp gates.
That evening, the generals sat in a plain room with metal beds and a single overhead light. Their military careers were over, their armies defeated, and their country’s future uncertain.
Von Keller took a notebook from his pocket and opened it to a blank page.
For years, he had filled its pages with maps, force estimates, and tactical observations. Now he wrote a different lesson:
An army can win an engagement with a superior weapon. A nation must sustain a war with everything that makes the weapon possible.
He closed the notebook.
Outside, the camp settled into silence. Somewhere across the ocean, American factories continued their work, turning steel, engines, labor, and carefully coordinated schedules into the equipment that sustained Allied operations.
The German generals had spent years measuring military strength by what they could see on the battlefield.
Inside that American factory, they had finally seen what stood behind it.
And they understood, too late to change the outcome of their war, that the decisive advantage was not always the tank rolling toward the enemy.
Sometimes, it was the factory already building the next one.